

Chromate Conversion Coatings for Aluminum (Chem Film) per MIL-DTL-5541
What is Alodine®? Also known as chem film or chemfilm, Alodine coating is a chromate conversion coating used to protect aluminum and other metals from corrosion while supporting electrical conductivity, paint adhesion, and dimensional stability. Related products include Iridite®, TCP-HF, Bonderite®, and Chromicoat®. The process of applying an Alodine® conversion coating or chromate conversion coating is referred to as chromating.
A chromate coating, often referred to as chem film, chemfilm, or Alodine® conversion coating, is widely used as a corrosion-resistant surface treatment for aluminum when electrical conductivity, paint adhesion, and dimensional stability are required. In many specifications and industries, chromate coating, chem film, and Alodine® are used interchangeably to describe this conversion coating process.
An Alodine coating is commonly specified when aluminum parts need corrosion protection without adding measurable thickness to the part surface. Because the coating is very thin, it can help protect the metal while preserving part dimensions, electrical conductivity, and compatibility with paint or primer. This makes Alodine coating useful for aluminum components that must remain conductive, paint-ready, or dimensionally stable after surface treatment.
The term Alodine coating is often used in shops and specifications to describe an Alodine® conversion coating or chem film finish. In practice, the right coating process depends on the required specification, material, application, and whether the part requires a Type I or Type II chromate conversion coating.
A chromate conversion coating, also called chem film or chemfilm, is a type of chemical conversion coating. During the chromate conversion coating process, the metal undergoes a chemical reaction at the surface. Unlike plating, which adds a new layer to the metal surface, a chromate coating transforms the existing metal surface into a protective layer via chemical reaction.
The use of a chromate coating is especially common in aerospace, defense, and electronics applications where corrosion resistance, electrical conductivity, and coating adhesion must be maintained without increasing part thickness. Because a chromate coating provides a thin, conductive barrier, it is widely specified for aluminum parts that must remain bondable, weldable, or paint-ready.
In addition to its functional benefits, a chromate conversion coating offers manufacturers a cost-effective and proven aluminum finishing solution that complies with military and industry standards such as MIL-DTL-5541, formerly known as MIL-C-5541. For applications where durability, reliability, and compatibility are critical, a chromate coating remains one of the most trusted surface treatments.
Modern chem film processes have evolved to meet today’s stricter environmental and performance requirements. Facilities often use trivalent chromium chem film formulations (Type II) instead of traditional hexavalent systems (Type I) to comply with RoHS and REACH regulations while maintaining corrosion protection and electrical conductivity. These advanced chem film coatings are especially valuable for aluminum components used in aerospace, military, and electronics applications where both compliance and performance are non-negotiable.
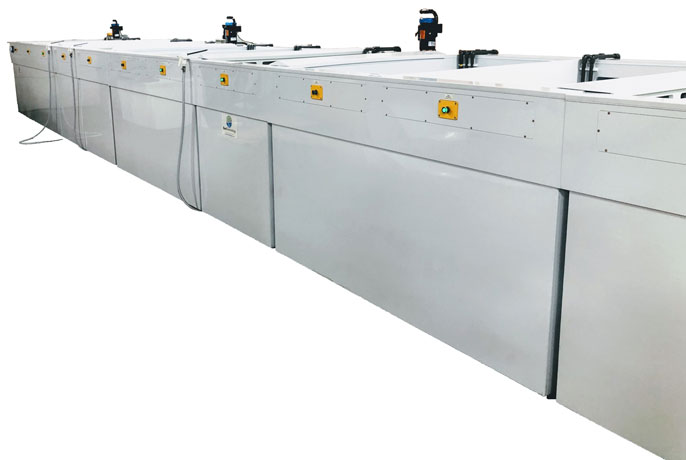
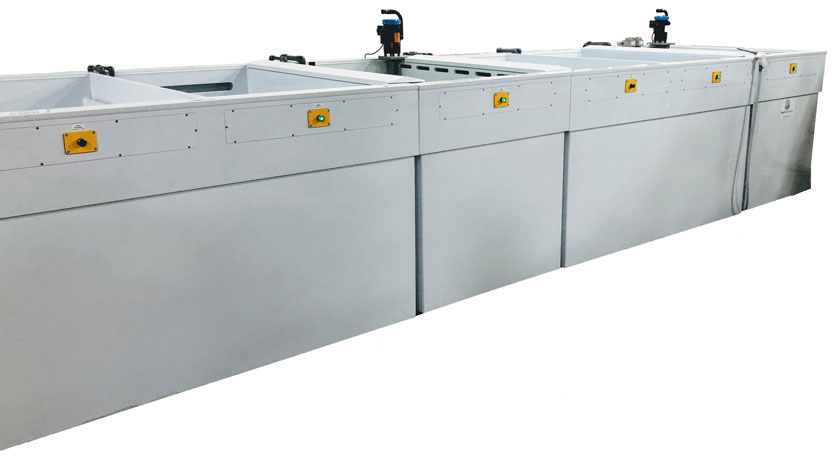
At Best Technology, our custom tank lines and automation systems are engineered to deliver consistent, high-quality chem film and chemfilm finishes for aluminum parts that require reliable corrosion protection and process control. Each system is designed to control parameters such as temperature, dwell time, and rinse quality—ensuring every part receives a uniform and reliable coating. Whether for small-batch R&D or full-scale production, our chem film equipment supports both Type I and Type II formulations, providing manufacturers with flexibility, precision, and long-term reliability.
Modern chromate coating technologies continue to evolve to meet both environmental and performance demands. The transition from hexavalent to trivalent chromium systems has allowed manufacturers to maintain corrosion resistance while reducing environmental impact. These newer formulations deliver excellent adhesion for paints and primers, making them ideal for aluminum structures in aerospace, defense, and electronics manufacturing. When properly applied, a chromate coating provides reliable conductivity and surface protection without compromising weldability or downstream finishing steps.
At Best Technology, we engineer complete processing lines that optimize every stage of the chromate coating application. From cleaning and etching to controlled immersion, rinsing, and drying, each system ensures precise film formation and repeatable results. Automated temperature control, dwell time monitoring, and conductivity-based rinse systems help guarantee uniform chromate coating performance across parts of varying geometries. The result is a consistent, specification-compliant finish that supports the long-term durability of critical aluminum components.
Benefits of Alodine®, Chem Film, and Chromate Conversion Coating
Compared to anodizing or plating, a chromate coating provides corrosion protection without building measurable thickness on the part. This makes chromate coating especially suitable for tight-tolerance aluminum components that must remain conductive, paint-ready, or prepared for secondary finishing operations.
For manufacturers, the value of a chromate coating is its ability to protect aluminum while preserving the surface characteristics needed for assembly, grounding, bonding, painting, or further finishing. This makes chromate coating a practical choice when corrosion resistance is required, but dimensional change must be minimized.
The primary benefit of an Alodine® conversion coating, also called chem film, is aluminum corrosion protection. But chromate coating with Alodine® offers other benefits. The chemical film leaves a base that provides better adhesion for organic coatings, and it can protect against the loss of electrical conductivity. Additionally, alodined aluminum surfaces provide excellent durability and reliability, making Alodine® conversion coating a preferred choice for aerospace and industrial applications. Alodining aluminum surfaces enhances their resistance to corrosion while maintaining conductivity, ensuring long-term performance in demanding environments.
A properly applied chemical film, often referred to as a chromate conversion coating or Alodine® conversion coating, enhances the surface integrity of aluminum without altering dimensional tolerances, making it ideal for tight-tolerance parts in aerospace and electronics. In many cases, chem film, also written as chemfilm, is used as a final finish on internal components or as a pretreatment before powder coating or painting. This makes Alodine® conversion coating useful when aluminum parts need corrosion protection, paint adhesion, and dimensional stability in the same process. The non-conductive or conductive properties of the chem film layer can be controlled depending on process parameters and specific product requirements, and these performance characteristics are one of the key reasons why chromate conversion coating remains a trusted choice across critical industries.
In addition to its performance advantages, chromate coating plays a critical role in meeting military and aerospace specifications, including MIL-DTL-5541. The specification outlines the standards for applying chromate conversion coatings to aluminum and its alloys to ensure corrosion protection and paint adhesion. In many of these applications, chem film is the preferred treatment process due to its reliability and compatibility with other surface finishes. When applied correctly, a chromate coating forms a thin, durable film that bonds tightly to the aluminum surface, offering long-term protection in aggressive environments.
From prototyping to full-scale production, chromate coating ensures that aluminum parts meet both functional and regulatory requirements. As environmental regulations evolve, manufacturers are also exploring trivalent chromium alternatives that still meet chromate conversion coating performance standards. These formulations aim to provide comparable corrosion resistance while reducing environmental and health impacts. Additionally, chem film offers a cost-effective solution when a durable yet low-profile surface finish is required.
What is Chem Film (Alodine®)? Video Overview
Chem Film Applications
Chromate conversion coatings (chem film) Alodine are used for heat sinks, automotive wheels, and everyday aluminum hardware and components. In aerospace applications, chromate conversion coatings chem film are used on aircraft hulls, including shock absorbers, side and torsion struts, landing gear, and flight control systems such as rudder systems and wing parts.
Chem film is especially critical for applications requiring both corrosion resistance and electrical conductivity in aluminum alloys used in harsh environments. Aluminum chromate conversion coating also ensures long-term durability, even in extreme operational conditions.
The Alodine process works by creating a protective chromate layer on aluminum surfaces, enhancing corrosion resistance while maintaining conductivity. This makes Alodine an essential surface finishing step for components that must withstand moisture, salt spray, and other environmental stresses.
Beyond aerospace, Alodine is widely applied in industries such as automotive, electronics, and general manufacturing. By improving paint adhesion and providing uniform surface protection, the Alodine process helps extend the life of aluminum parts while ensuring they meet strict industry standards for performance and reliability.
Chem Film or Alodine Process and Benefits
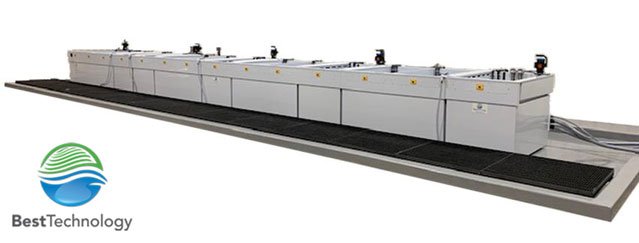
Alodine Equipment for Applying Chromate Conversion Coatings
Types of Chromate Conversion Coating (Chem Film)
The MIL-DTL-5541 specification, Chemical Conversion Coatings on Aluminum and Aluminum Alloys, is the most commonly used specification for chem film, Alodine®, and chromate conversion coating on aluminum. This standard was previously designated MIL-C-5541, and the older name is still frequently used in drawings, purchase orders, and manufacturing documentation. MIL-DTL-5541 distinguishes between different types and classes of conversion coating based on chemistry, corrosion protection, electrical conductivity, and final application requirements. The Type depends on the chemical composition of the coating material, while the Class relates to its intended purpose. Alodining aluminum surfaces is a widely used process to achieve compliance with MIL-DTL-5541 standards. Chromate conversion coating ensures compliance with MIL-DTL-5541 standards for both Type 1 and Type 2 processes, providing corrosion resistance and improved adhesion for subsequent coatings.
For Types, the MIL-DTL-5541 standard defines two types of chemical conversion coating for aluminum, based on the presence or absence of hexavalent chromium in the coating.
How Chem Film Supports MIL-DTL-5541 Requirements
Chem film supports MIL-DTL-5541 requirements by creating a protective conversion coating on aluminum and aluminum alloys. This coating helps improve corrosion resistance while also preparing the surface for paint, adhesive bonding, or other finishing steps. For manufacturers working to MIL-DTL-5541 standards, chem film is commonly used because it provides both surface protection and process compatibility.
The right chem film process depends on the required MIL-DTL-5541 type and class. Type 1 uses hexavalent chromium chemistry, while Type 2 uses hex-free alternatives such as trivalent chromium, titanium, or zirconium-based coatings. In both cases, the goal is to apply a controlled chromate conversion coating that supports the required performance, appearance, and compliance needs for the application.
When a drawing or purchase order calls for an Alodine coating, the manufacturer should confirm the required type, class, chemistry, performance requirement, and applicable specification before processing parts. These details affect the conversion coating chemistry, tank sequence, dwell time, rinse quality, inspection method, and documentation needed for the finished aluminum component.
For manufacturers building or upgrading a chem film line, MIL-DTL-5541 should be considered at the process-design stage, not only during final inspection. Tank material, cleaning, deoxidizing, conversion coating dwell time, rinse quality, drying, ventilation, and waste handling can all affect whether the finished aluminum parts meet the required type, class, and performance expectations.
MIL-DTL-5541 Type 1
MIL-DTL-5541 Type 1 contains hexavalent chromium, also known as hex chrome. This was the customary process for many years, and was used until safer chemicals were introduced.
Exposure to hexavalent chromium is now tightly regulated in the United States by both the EPA, as an environmentally hazardous chemical, and by OSHA, as a carcinogenic chemical. If using Type 1 for MIL-DTL-5541 spec work, be sure to check with your state or county for processing permits that pertain to proper venting and disposal of hex chrome. Chromate conversion coating systems for Type 1 applications often require advanced ventilation and disposal solutions to meet regulatory requirements.
MIL-DTL-5541 Type 2
MIL-DTL-5541 Type 2 is known as hex-free chromating. In this type the hexavalent chromium has been replaced with trivalent chromium, titanium or zirconium, and it is typically accepted as the standard across many industries. Best Technology partners with Chemeon, an industry leader in hex-free trivalent chromium coating chemistries, to offer a hex-free product named TCP-HF (hexavalent free) that has approvals for many aerospace and military applications.
The hex-free coating can result in a faint blue color appearing almost unchanged from bare material. eTCP is a colored version of TCP-HF developed to exhibit visual identification for quality control purposes.

Advancements in trivalent chromate coating on aluminum allow the trivalent process to have many benefits over Type 1:
- Faster to apply
- Room temperature to apply. This saves on electrical energy that would otherwise be needed to heat the tanks. Lack of heated tanks also eliminates concerns about evaporative losses.
- Fewer process steps (typically 5 steps vs. 9 steps for hexavalent chromium, Type 1)
The development of trivalent chem film has also helped industries transition to safer and more environmentally friendly solutions while maintaining strict performance standards.
Classes of Chromate Conversion Coating (Chem Film)
The Class of a chemical film coating depends on its intended purpose. The MIL-DTL-5541 spec describes two classes of chromate coating that are commonly used in chemical film applications.
MIL-DTL-5541 Class 1A
Class 1A: This class of chromate coating on aluminum tends to be much thicker than other classes, as well as darker, which provides a high grade of corrosion protection for unpainted items. It also improves adhesion of paint finish systems on aluminum and aluminum alloys. The military uses chemical agent-resistant coating (CARC) paint on a wide variety of vehicles and equipment as added protection against chemical agents.
MIL-DTL-5541 Class 3
Class 3: This class of chromate coating on aluminum has two objectives: It is designed not only to protect against corrosion, but also to reduce interference with electrical conductivity. These coatings are usually thinner than Class 1A, and they have a lighter coating weight. Alodine conductivity is technically an incorrect term as the coating itself is not conductive; rather, the Class 3 coating is thin enough to permit the aluminum to retain its conductivity.
The following chart summarizes the key differences between the Types and Classes of chromate conversion coatings according to the MIL-DTL-5541 standard. The specification is also commonly searched for and referenced by its former designation, MIL-C-5541, particularly in older engineering drawings and procurement documents.
MIL-DTL-5541 Types and Classes for Chromate Conversion Coating
| MIL-DTL-5541 Standard | Type 1 | Type 2 |
| Chromates | Hexavalent Chromate | Hex-Free Chromate (Trivalent Chromate) |
| Class 1A | Maximum corrosion protection | Maximum corrosion protection |
| Class 3 | Improved electrical conductivity with corrosion protection | Improved electrical conductivity with corrosion protection |
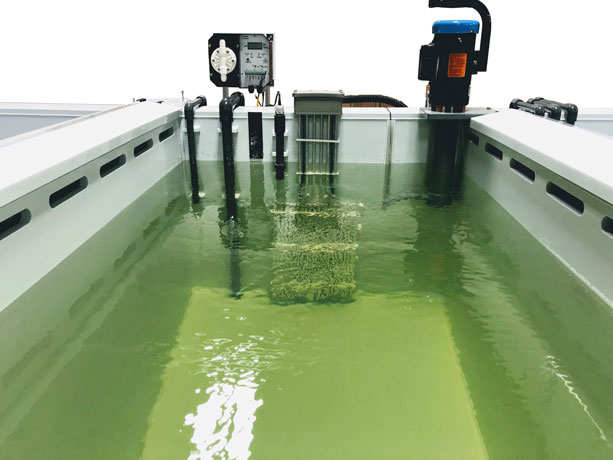
Alodine Chemical Conversion Coating Tank
Alodine Process for Aluminum Treatment
The chemical film / Alodine process steps vary for Type 1 vs. Type 2. The Type 2 chemical conversion coating process allows for use of either an alkaline or acid cleaner. Though the time varies according to the part and process type, it typically takes each part ten minutes to a half-hour to produce an Alodine coating or chromate coating on aluminum. Newer aerospace cleaning protocols recommend a pretreatment step before chromate conversion to improve surface adhesion.
Type 1 Chromating Process
The Type 1 hexavalent chromate conversion coating process (Alodine process) includes 9 process steps.
- Clean: A general washing in a cleaning solution takes place as a pre-process step. This ensures that dirt, oil, and any residue formed from prior manufacturing or packaging processes is removed before the chromate coating begins. Then a rinse and dry takes place.
- Rinse: Ensure any alkaline detergents are removed from the part. A water-break-free test is often performed.
- Etch: If there are any areas that the chem film coating should not be applied to, the etching process covers those areas.
- Rinse: Ensure any etching chemistry is rinsed to stop the etching process.
- Deox: Deoxidation of the part occurs next, to remove any excess materials and oxides, contaminants and chemicals.
- Rinse: Remove any deox solution.
- Chem film coat: The surface conversion process takes place when the aluminum is immersed in the tank. The chromate conversion coating gets applied immediately. The period of time that it remains in immersion varies based on the method of the application, the composition of the chemical film and the composition and size of the part itself.
- Rinse.
- Warm rinse.
Video: Chem Film/Chromate Conversion Alodine and Passivation 14-Tank Line

Type 2 Chromating Process
The Type 2 hex-free chem film process for surface conversion (chromate conversion) with TCP-HF has two variations, Acid Clean and Alkaline Clean.
Acid Clean Chem Film process
- Acid Clean
- Rinse
- Trivalent chromium, hex-free chrome coat
- Rinse
- Second Rinse is used in the Type 2 method of surface conversion coating known as TCP-HF.
The alternative Type 2 hex-free chem film process for conversion is known as Alkaline Clean process.
Alkaline Clean Chem Film process
- Alkaline Clean
- Rinse
- Deox
- Rinse
- Trivalent chromium, hex-free chrome coat
- Rinse
- Second Rinse is used in the Type 2 method of surface conversion coating known as TCP-HF.
It’s important to deoxidize the part prior to trivalent chrome processing. While deoxidizing is inherent in the Type 2 Acid Clean Chem Film process, the Type 2 Alkaline Clean process requires 2 additional steps to deoxidize and rinse the part prior to trivalent chrome processing.
Best Technology offers equipment for Type 1 or Type 2 chromate conversion coatings.
Type 2 Chem Film / Chromate Conversion Coating Tank System

Testing per MIL-DTL-5541 Specification
Testing for MIL-DTL-5541 chem film applications commonly includes corrosion-resistance validation using salt-fog testing on representative panels. Test cycles are often run for 168 hours in a salt-fog chamber using a five-percent salt spray, depending on the required type, class, and customer specification. Because this testing is destructive, manufacturers typically use test panels rather than production parts to verify that the chromate conversion coating process remains in control.
Process validation for chromate conversion includes testing for salt-spray performance, adhesion, and electrical conductivity. Organizations that require NADCAP certification (National Aerospace and Defense Contractors Accreditation Program) often perform internal audits on chromate coating documentation and traceability.
Whether applied manually or with automated chem film application systems, chemical film coatings remain one of the most efficient and widely accepted solutions for aluminum surface protection in critical industries.
Standards and Specifications for Conversion Coatings
| Standard | Title / Description |
| MIL-DTL-5541 |
Military Specification, Chemical Conversion Coatings on Aluminum and Aluminum Alloys
|
| MIL-DTL-81706 |
Military Specification, Chemical Conversion Materials for Coating Aluminum and Aluminum Alloys
|
| ASTM B449 |
Standard Specification for Chromates on Aluminum
|
| ASTM B921 |
Standard Specification for Non-hexavalent Chromium Conversion Coatings on Aluminum and Aluminum Alloys
|
| AMS 2473 |
Chemical Film Treatment for Aluminum Alloys, General Purpose Coating
|
| AMS 2474 |
Chemical Treatment for Aluminum Alloys, Low Electrical Resistance Coating
|
| ISO 8081 |
Aerospace process, Chemical conversion coating for aluminum alloys, General purpose
|
| BAC 5719 |
Chemical Conversion Coatings for Aluminum and Aluminum Alloys
|
Chromate Coating Equipment for Aerospace

Common Applications for Chem Film Coatings
What is a conversion coating used for? Chem film is widely used in industries that require both corrosion resistance and electrical conductivity, such as aerospace, defense, and electronics manufacturing. Because chem film coatings do not significantly alter part dimensions, chromate conversion coating is ideal for precision applications where tight tolerances are required. This makes chem film a cost-effective and efficient solution for protecting aluminum components while ensuring compliance with industry standards.
An Alodine coating is often selected when manufacturers need corrosion protection without significantly changing part dimensions. This makes it useful for aluminum components that must maintain tight tolerances, electrical conductivity, paint adhesion, or grounding performance after surface treatment.
- Aerospace: The high speed of aircraft travel coupled with atmospheric gases at extremely high altitudes contributes to corrosion of aircraft parts. As a result maximum protection is necessary for as many parts as possible. Even passing through clouds can cause corrosion of aircraft parts. Aluminum corrosion protection is critical to aerospace metal finishing applications and an Alodined or aluminum chromate-coated aerospace part can prevent surface exposure to such elements. Emerging aerospace programs continue to specify chromate coating for aluminum chassis and brackets that must pass both vibration and corrosion tests.
- Maritime/Naval: Watercraft, large and small, need to be as resistant to corrosion as possible. Boat interiors and mechanical parts can be impacted by water damage, especially boats meant to be in saltwater. Conversion coating allows parts to withstand corrosive saltwater environments and pass salt-spray testing methods. The anti-corrosive properties of chemical films are in high demand for this purpose. The chromate coating’s qualities as a paint primer can be useful here too, for custom colors on watercraft.
- Military and defense: The U.S. Department of Defense uses chemical film in a variety of ways. Such a large number of military parts are primed and protected with Alodine chem film coating, that the U.S. military has created a standard for the finishing method, with detailed specifications. The standard MIL-DTL-5541 regulates the chem film chemical coating treatment and places chemical conversion coatings into categories based on their applications. Brushed-on chem film is also used to repair surfaces and components that have been anodized.
- Electrical industry: Electricians appreciate the chromate coating corrosion protection when they apply a surface conversion coating to wire housing, which holds and/or protects wiring. This helps to prolong the life and performance of the wires. Alodine coatings in the electrical industry provide not only corrosion protection to wire housings and panels but also reduction of electrical conductivity losses. The use of chromate conversion in precision components is often preferred due to its compatibility with temperature-sensitive adhesives and coatings.
- Other industries such as telecommunications, medical device manufacturing, and precision electronics also rely on chromate coating for surface integrity and electrical performance. Because these applications often demand consistent conductivity and minimal surface alteration, chromate conversion coating remains a preferred surface treatment method. The use of chem film in these sectors ensures minimal dimensional change while enhancing corrosion resistance. The process offers flexibility in application—ranging from immersion lines to manual brush applications—allowing manufacturers to tailor the coating method to their production needs.
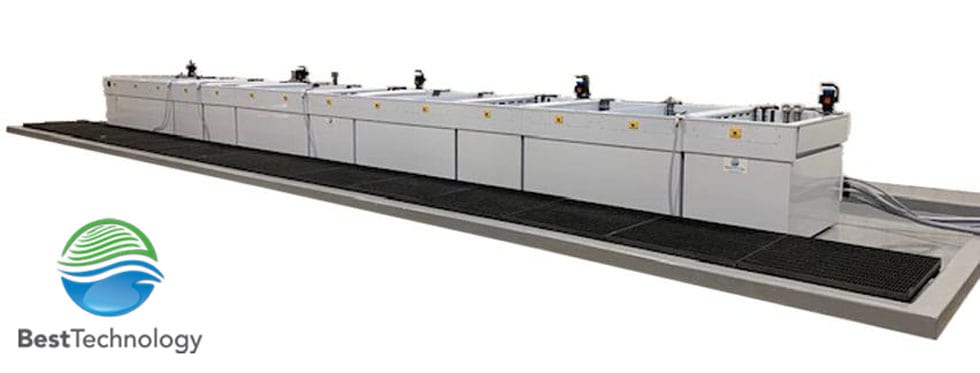
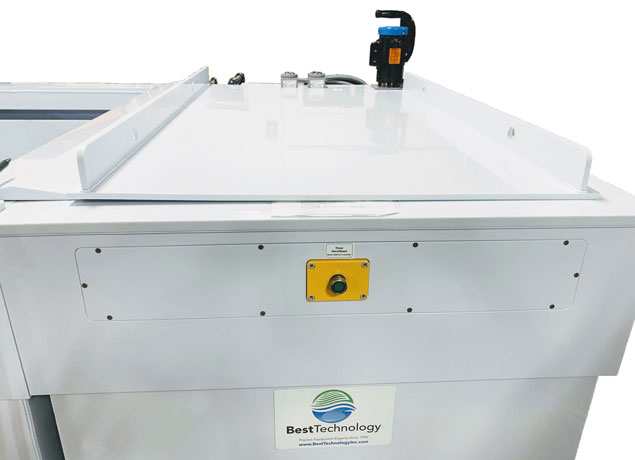
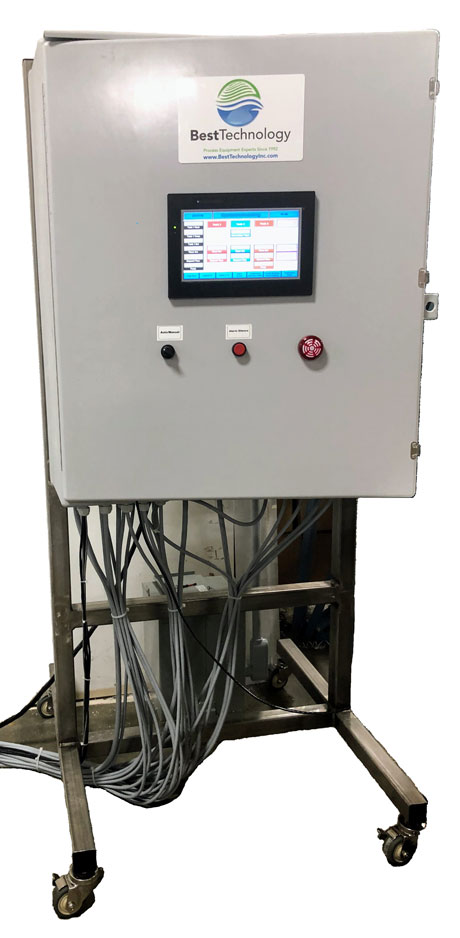
Chem Film Equipment for Alodine-Treated Aluminum
Chem Film Coating Best Practices
The quality of the material, and the material type, go a long way to determine the outcome of the surface conversion. Variations in the purity or overall quality of the material, will affect the final appearance after the Alodine process steps. The class of the chemical film will also have an effect on the chromate finish: Class 1A chem film is thicker and darker than the lighter, thinner Class 3 chem film.
The preparation stages of chromate conversion coatings are important too. Ineffective rinses can lead to contaminated tanks. Improper acid activation or pH levels in tanks can reduce quality of the results. Allow the experts at Best Technology to handle the details and build a chem film line for you, so that parts get cleaned and your chromate conversion coating process meets the highest standards.
Chem Film / Alodine / Chromate Conversion FAQs
-
What is aluminum chromate conversion coating?
A chromate conversion coating is a type of chemical conversion coating that is typically applied to aluminum alloys. Other types of chemical conversion coatings include iron phosphate and zinc phosphate coatings, typically applied to steel.
A chromate conversion coating protects the underlying aluminum against corrosion, serves as a base for paint adhesion, and can allow for electrical conductivity when applied as a thin coat.
Chromate coating on aluminum is widely used in the aerospace industry, as well as with everyday hardware such as nuts and bolts.
-
What is chem film?
Chem film, also called chemical film, is a chemical conversion coating. It typically refers to a chromate conversion coating applied to aluminum and its alloys. The chemfilm coating provides a layer of corrosion protection and a base for paint and primer. When applied as a thin coat, chem film can allow for electrical conductivity.
Chem film coatings are marketed under brand names such as Alodine®, Iridite® and Chromicoat®.
The chemfilm coating process is often governed by the commonly used MIL-DTL-5541 standard, which specifies different types and classes of chem film coatings.
Current Trends in Chem Film Adoption
With global regulations tightening around hexavalent chromium, many facilities are upgrading their lines to trivalent alternatives while still relying on Chem Film for proven adhesion and corrosion resistance. Aerospace OEMs, in particular, have rewritten finishing specs to mandate periodic verification that Chem Film thickness and contact resistance remain within tolerance.
Integrating Chem Film Into Hybrid Finishing Cells
Modern plating shops now combine anodizing, powder coating, and Chem Film pretreatment within a single production cell. This hybrid approach shortens lead times, reduces handling damage, and ensures a consistent chemical conversion layer before paint or primer application.
-
Is Alodine conductive?
What is the electrical conductivity of chromate conversion coatings, also called Alodine® or chem film, when applied to aluminum alloys?
Unlike anodizing, Alodine coatings offer electrical conductivity for aluminum parts, when applied according to Class 3 of the MIL-DTL-5541 standard. Class 3 chemical conversion coatings protect against corrosion where low electrical resistance is required.
Coating Thickness
Because Class 3 coatings are thinner, they provide less corrosion resistance than Class 1A, but the trade-off is better electrical conductivity.
Technically the coating itself is not conductive, but rather the Class 3 coating is thin enough to allow the aluminum to retain its electrical conductivity.
Surface Roughness
The other factor that affects Alodine conductivity is surface roughness. A rougher surface finish allows greater conductivity due to breaks in the coating. In contrast, highly polished surfaces have lower conductivity due to lack of breaks in the coating.
To meet the Class 3 MIL-DTL-5541 standard, parts must have electrical resistance of no more than 0.005 – 0.010 ohms per square inch under nominal electrode pressure of 200 psi with a flat contact.
Applications
Common applications for electrically conductive Alodine coatings include parts that need to be electrically grounded.
In addition to electrical conductivity, Alodine coatings offer thermal conductivity and are used in applications such as heat sinks.
Chromate conversion coatings such as Alodine are an effective solution for aluminum alloys when both corrosion resistance and conductivity are important.
-
Alodine vs. Anodize: What’s the difference?
Wondering about the difference between chem film vs anodize?
The primary difference between Alodine (chem film) and anodizing is that anodizing is an electrolytic process, while Alodine is a chemical conversion coating process that does not require electrical current.
Alodine (chem film) and anodizing are both aluminum finishing processes used to improve corrosion resistance. Each process modifies the outer surface of the metal, but they create different coatings and provide different functional properties.
But Alodine (chem film) and anodizing are NOT the same.
Anodizing is an electrolytic finishing process that applies electrical current to aluminum while it is immersed in an electrolyte solution. In addition to improving corrosion resistance, anodizing can provide better lubrication or allow the surface to be dyed. It is generally more expensive and technically complex than applying an Alodine chem film coating.
In contrast, Alodine (chem film) coatings do not require electrical current. The aluminum is typically immersed in a chemical bath, often at room temperature. Compared with anodizing, chem film is generally less expensive and requires less technical expertise. It can also allow aluminum to retain electrical or thermal conductivity, making Alodine a preferred option when finished parts must remain electrically grounded.
Best Technology offers equipment for Alodine (chem film) and titanium anodizing, but we do not currently offer equipment for aluminum anodizing.
-
What is chemical conversion coating?
A chemical conversion coating is a surface treatment applied to metals in which the metal undergoes a chemical reaction at the surface. This chemical reaction transforms the metal surface into a thin protective layer.
When applied to aluminum, a chemical conversion coating is sometimes called an aluminum conversion coating.
Chemical conversion coatings provide increased corrosion resistance and a uniform, inert surface for powder coating or paint adhesion.
A chemical conversion coating can also improve electrical conductivity and prepare metal surfaces for subsequent processes such as anodizing or sealing. It plays a critical role in industries like aerospace, electronics, and defense, where consistent surface quality is essential.
Chemical conversion coatings are typically applied via immersion in a chemical tank or bath, or by brushing or spraying. Proper process control—such as monitoring bath concentration, temperature, and immersion time—is important to achieve uniform results and ensure coating performance.
Routine inspection and testing of a chemical conversion coating help verify thickness, adhesion, and corrosion resistance. Maintaining a balanced bath ensures each chemical conversion coating performs consistently and meets industry specifications.
The versatility of a chemical conversion coating makes it a preferred choice for manufacturers who require both corrosion protection and surface preparation in a single process.
Types of chemical conversion coatings vary according to the metal substrate:
-
Iron phosphate coatings – Used with steel
-
Zinc phosphate coatings – Used with galvanized steel
-
Chromate conversion coatings – Used with aluminum alloys
By selecting the appropriate chemical conversion coating, manufacturers can improve durability, corrosion resistance, and paint adhesion across a wide range of metal components.
Best Technology offers phosphating tank lines for iron phosphate coatings and zinc phosphate coatings, and Alodine tank lines for chromate conversion coatings. Our chemical department offers trivalent chromate conversion coating chemistry for use on aluminum alloys.
-
Other Materials Protected from Corrosion by Chem Film
While aluminum is what is typically used for chemfilm, other metal alloys such as copper, magnesium, cadmium and tin also benefit from the protection against corrosion that chromate conversion coating offers.
Steel and iron are not compatible with chem film when applied directly. But zinc-plated steel can be treated with chemfilm to achieve added durability and protection against white corrosion. On iron substrates, a chromate conversion coating can be added to improve the durability of a phosphate conversion coating.
Aluminum Corrosion Treatment Products
| Product | Manufacturer | Sample Products | Chemistry |
| Alodine | Henkel | Alodine 1200S, Alodine 1201, Alocrom 1200 (U.K.), Alodine 1132 pen, Alodine 600 |
Chromate conversion coating for aluminum, contains hexavalent chromium. Resulting color is iridescent gold or yellow to tan. Also known as yellow chromate. |
| Alodine 1000 clear, Alodine 1001 clear, Alodine 1500 clear |
Chromate conversion coating for aluminum, contains hexavalent chromium. Resulting color is clear. Also known as clear chromate or clear chem film. | ||
| Alodine 871 | Non-hexavalent (hex-free) chromium conversion coating for aluminum | ||
| Alodine 5200, Alodine 5700 |
No-Chromium (hexavalent or trivalent) alternative treatment for aluminum or magnesium. | ||
| Iridite | Macdermid | Iridite 14-2 | Chromate conversion film for aluminum and its alloys |
| Iridite 15 | Chromate conversion treatment for magnesium and its alloys | ||
| Iridite NCP | No-Chromium (hexavalent or trivalent) alternative to chromate-based treatments for aluminum | ||
| Bonderite | Henkel | Bonderite 1020, Bonderite 1030 |
Iron phosphate conversion coatings for application to steel surfaces |
| Bonderite 3410 | Zinc phosphate conversion coating for application to steel, zinc and aluminum | ||
| Bonderite NT-1 | Zirconium-based, non-phosphate alternative to traditional iron phosphate, for application to steel, zinc, and aluminum | ||
| Chromicoat | Chemetall | Chromicoat L25 | Chromate conversion coating for aluminum, contains hexavalent chromium |
| TCP-HF (Hexavalent free) | Chemeon | TCP-HF, eTCP |
Trivalent chromium (hex-free) conversion coating for application to aluminum, magnesium, zinc, zirconium and other alloys |
Video: Chem Film Chromate Conversion Type 1 System

For manufacturers seeking both corrosion resistance and surface conductivity, chromate conversion coating offers a reliable solution that meets MIL-DTL-5541 standards. When applied as a standalone treatment or as a pre-paint adhesion promoter, chromate conversion coating delivers consistent, high-performance protection for aluminum components in aerospace, defense, and electronics applications.
Whether your needs are Type 1 or Type 2 (TCP-HF), call on Best Technology for all of your chemical conversion coating equipment needs. Bring your aluminum chromating process in-house, and get a chromate conversion coating system from Best Technology. Contact us today for a free quote.

 612.392.2414


