Best Technology

Precision Cleaning, Passivation & Finishing Systems

Call Us612.392.2414
Contact an Expert
  • Equipment
    • Industrial Parts Washers
    • Ultrasonic Cleaning Systems
    • Vapor Degreasing Systems
    • Passivation Equipment
    • Electropolishing Equipment
    • Chem Film Equipment
    • Titanium Anodizing Systems
    • Mass Finishing Machines
    • Automation Systems
    • Wet Benches
    • Specialty & Custom Industrial Process Systems
  • Chemicals
    • Chemicals, Solvents & Fluids
    • BestSolv® Engineered Fluids
    • 3Mâ„¢ Novecâ„¢ Replacement Fluids
    • 3Mâ„¢ Novecâ„¢ Engineered Fluids, Chemicals, & Solvents
    • 3Mâ„¢ Novecâ„¢ HFE Engineered Fluids and PFAS Phase Out
  • Industries
  • Articles
    • FAQ – Frequently Asked Questions
    • Ultrasonic Cleaning
      • How Do Ultrasonic Cleaners Work?
    • Passivation
      • What is Passivation?
    • Electropolishing
      • What is Electropolishing?
    • Surface Finishing
      • What is Alodine® / Chem Film / Chromate Conversion Coating?
      • What is Titanium Anodizing?
    • Industrial Parts Washers
    • Automation Systems
  • Case Studies
    • Industry Applications
    • Industrial Parts Washer Case Studies
    • Passivation Systems Case Studies
    • Part Cleaning Case Studies
    • Part Finishing Equipment Case Studies
    • Ultrasonic Cleaning Systems Case Studies
  • Testimonials
  • About Us
  • Contact Us
  • Equipment
    • Industrial Parts Washers
      • Products
        • Agitated Immersion Heated Parts Washer
        • Automatic Parts Washer System with Conveyor
        • Phosphating Lines
        • Automated Phosphate Lines for High-Volume Powder Coat Pre-Treatment
        • Oil Removal Systems
      • Case Studies
        • Pipe Washing Equipment
        • Designing a Phosphate Line for Today’s Process and Tomorrow’s Needs
        • Machine Shop Parts Washer for True Oil
        • Automotive Parts Washer System
    • Ultrasonic Cleaning Systems
      • Product Information
        • How Clean is Clean?
        • How Do Ultrasonic Cleaners Work?
        • What is an Azeotrope?
      • Products
        • Benchtop Ultrasonic Cleaner
        • Benchtop Ultrasonic Parts Cleaning Multi-Tank Systems
        • Ultrasonic Cleaning Consoles
        • Automated Ultrasonic Parts Cleaning Equipment Wash-Rinse-Dry
        • Automated Ultrasonic Cleaning System for High-Volume Production
        • Large Ultrasonic Parts Cleaner with Agitated Immersion
        • Immersible Ultrasonic Transducers
        • Vapor Degreasing Systems
        • Vapor Degreasers
      • Case Studies
        • Automated Pickling and Cleaning System Case Study
        • Automated Ultrasonic Injection Mold Cleaner System
        • 3D Printer / FDM Parts Post Process Ultrasonic Cleaning
        • Machine Shop Parts Washer for Swiss and CNC Precision Parts
        • Vapor Degreaser For Medical Device Instruments
    • Passivation Equipment
      • Product Information
        • What is Passivation? How Does It Work?
        • Nitric vs. Citric Acid Passivation
        • Passivation with Citric Acid
        • What Is Pickling of Stainless Steel? How Do Descaling, Pickling and Etching Work?
        • Passivation Cost Savings Calculator
      • Products
        • Benchtop Ultrasonic Passivation Equipment
        • Passivation Wet Bench for Citric / Nitric Acid
        • Ultrasonic Automated Passivation Equipment
        • Automated Passivation Systems for High-Volume Production
        • Agitated Immersion Multi-Tank Passivation Systems
        • Salt Fog and Humidity Test Chambers for Reliable Corrosion and Environmental Testing
      • Case Studies
        • Case Study: Bringing Citric Acid Passivation In-House for Stainless Steel Medical Device Parts
        • Automated Ultrasonic Passivation System for Medical Device Parts
        • Cleanroom Space Saving Automated Passivation System
        • Heated Polypropylene Acid Passivation and Rinse Tanks
        • Applicable Articles
    • Electropolishing Equipment
      • Product Information
        • What is Electropolishing? How Does Electropolishing Work?
        • Electropolishing Cycle and Current Calculator
        • Passivation vs. Electropolishing
      • Products
        • Tabletop Electropolishing Equipment & Electropolishing Machines
        • Electropolishing Wet Benches
        • Semi-Automated Electropolishing Systems for High-Volume Production
        • Large Scale Part Electropolishing Systems
      • Case Studies
        • EP System – Open Top Wet Bench with Spray Rinse
    • Surface Finishing Systems
      • Chem Film Equipment / Alodine Lines
        • Chem Film Equipment
        • What is Alodine / Chem Film / Chromate Conversion Coating?
        • Alodine Chem Film Tank Line
        • Ready to Set Up a Chem Film (Alodine) Line?
        • Automated Chem Film (Alodine) Systems
        • Hex Chrome Phase Out and Alternatives for Conversion Coating
        • Salt Fog and Humidity Test Chambers for Reliable Corrosion and Environmental Testing
      • Mass Finishing Machines
        • Centrifugal Barrel Finishing Machines
        • Vibratory Bowl Polishers
      • Titanium Anodizing
        • Titanium Anodizing Systems
        • What is Titanium Anodizing?
        • Titanium Anodizing Equipment
    • Automation Systems
      • Product Information
        • What Is Process Automation for Metal Finishing?
      • Products
        • Rail-Mounted Gantry Crane Automation
        • Automated Passivation Systems for High-Volume Production
        • Automated Ultrasonic Cleaning System for High-Volume Production
        • Automated Chem Film (Alodine) Systems
        • Semi-Automated Electropolishing Systems for High-Volume Production
        • Automated Phosphate Lines for High-Volume Powder Coat Pre-Treatment
        • Ultrasonic Automated Passivation Equipment
      • Case Studies
        • Automated Pickling and Cleaning System Case Study
        • Automated Passivation for High-Volume Production: Case Study
    • Wet Benches
      • Product Information
        • What is a Fume Hood? How Do Fume Hoods Work?
      • Products
        • Fume Hoods
        • Wet Bench for Semiconductor & FM4910 Applications
        • Wet Benches for Citric / Nitric Passivation of Stainless Steel and Titanium
        • Wet Benches for Electropolishing
        • Cascade Overflow Rinse Tanks
        • Quick Dump Rinse Tank
      • Case Studies
        • Semiconductor Chemical Processing Wet Bench and Fume Hood
    • Specialty & Custom Industrial Process Systems
      • Automated Chemical Neutralization Tank Cart
      • Salt Fog and Humidity Test Chambers
      • Vapor and Dryfilm PTFE Coating Systems
      • Heated Hot Air Parts Dryer
      • Solvent Recovery Equipment
    • Process Validation Templates
    • Equipment Financing
  • Chemicals, Solvents & Fluids
    • Chemicals, Solvents & Fluids from Best Technology
    • BestSolv® Engineered Fluids
    • Solvent Cleaning Fluids
      • Solvent Cleaning with BestSolv® Engineered Fluids
      • BestSolv® Alpha
      • BestSolv® Bravo
      • BestSolv® Delta
      • BestSolv® Echo
      • BestSolv® Lima
      • BestSolv® Omega: PFAS Free
      • BestSolv® Omega Plus: PFAS-Free
      • BestSolv® Sierra
      • BestSolv® Theta
      • BestSolv® Zeta: PFAS-Free
      • BestSolv® 5408: Boeing Spec BAC 5408 Qualified Cleaning Solvent
      • BestSolv® 7100
      • BestSolv® 7200
      • BestSolv® 7300
      • BestSolv® 71DE
      • BestSolv® 72DA
      • BestSolv® 72DE
      • BestSolv® 73DE
      • BestSolv® nPB: TCE Replacement
      • Latent Fingerprint Processing with BestSolv® Engineered Fluids
      • What Are Hydrofluoroether (HFE) Fluids?
      • Film Cleaning with BestSolv® 7200
      • Oxygen System and Oxygen Gauge Cleaning Solutions
      • Carrier Fluids for Precision Deposition, Wetting, and Material Transport
      • Choosing the Best Vapor Degreaser Solvent
    • Thermal Management / Heat Transfer Fluids
      • Thermal Management / Heat Transfer with BestSolv® Engineered Fluids
      • BestSolv® Zulu Immersion Cooling Fluid
      • BestSolv® Zulu MAG Magnesium Protection Fluid
      • BestSolv® Zulu FS Fire Suppression Fluid
      • BestSolv® 7100
      • BestSolv® 7200
      • BestSolv® 7300
      • BestSolv® 3283
      • BestSolv® 40
      • BestSolv® Fluids as Coolants for Specialized Machinery and Chiller Systems
      • Magnesium Cover Gas, Re-Engineered for Today
      • Gross Leak Testing for Hermetic Components and Critical Assemblies
    • PFAS-Free Next Generation
      • BestSolv® Omega: PFAS-Free
      • BestSolv® Omega Plus: PFAS-Free
      • BestSolv® Zeta: PFAS-Free
      • PFAS-Free Cleaning Solvents for Vapor Degreasing Applications
      • BestSolv® HFO / HCFO Solvents for Precision Cleaning
    • 3Mâ„¢ Novecâ„¢ Replacements
      • 3Mâ„¢ Novecâ„¢ Replacement Fluids
      • 3Mâ„¢ Novecâ„¢ 7100 Replacements
      • 3Mâ„¢ Novecâ„¢ 7200 Replacement
      • 3Mâ„¢ Novecâ„¢ 7300 Replacement
      • 3Mâ„¢ Novecâ„¢ 71DA Replacements
      • 3Mâ„¢ Novecâ„¢ 71DE Replacement Options
      • 3Mâ„¢ Novecâ„¢ 71IPA Replacements
      • 3Mâ„¢ Novecâ„¢ 72DA Replacements
      • 3Mâ„¢ Novecâ„¢ 72DE Replacements
      • 3Mâ„¢ Novecâ„¢ 73DE Replacement
      • Running Out of 3Mâ„¢ Novecâ„¢ Stock? How to Transition to Your BestSolv® Replacement Path
    • 3Mâ„¢ Novecâ„¢ Engineered Fluids and Fluorinertâ„¢ Liquids
      • 3Mâ„¢ Novecâ„¢ Engineered Fluids
      • 3Mâ„¢ Novecâ„¢ HFE Engineered Fluids and PFAS Phase Out
      • 3Mâ„¢ Novecâ„¢ Cleaning Solvents
        • Solvent Cleaning with 3Mâ„¢ Novecâ„¢ Engineered Fluids
        • 3Mâ„¢ Novecâ„¢ 7100
        • 3Mâ„¢ Novecâ„¢ 7200
        • 3Mâ„¢ Novecâ„¢ 7300
        • 3Mâ„¢ Novecâ„¢ 71DA
        • 3Mâ„¢ Novecâ„¢ 71DE
        • 3Mâ„¢ Novecâ„¢ 71IPA
        • 3Mâ„¢ Novecâ„¢ 72DA
        • 3Mâ„¢ Novecâ„¢ 72DE
        • 3Mâ„¢ Novecâ„¢ 73DE
      • 3Mâ„¢ Fluorinertâ„¢ and 3Mâ„¢ Novecâ„¢ Heat Transfer and Thermal Management Fluids
        • 3Mâ„¢ Fluorinert™ Electronic Liquids for Thermal Management / Heat Transfer
        • 3Mâ„¢ Novecâ„¢ 649
        • 3Mâ„¢ Novecâ„¢ 7100
        • 3Mâ„¢ Novecâ„¢ 7200
        • 3Mâ„¢ Novecâ„¢ 7300
    • Solvent Phase Outs
      • 3Mâ„¢ Novecâ„¢ HFE Engineered Fluids and PFAS Phase Out
      • nPB Replacement
      • TCE Replacement
      • Methylene Chloride Replacement
    • Aqueous Cleaning
      • Aqueous Cleaning Solutions: Alkaline Cleaners
      • How Clean is Clean?
    • Surface Finishing Chemicals
      • CitriSurf Passivation Chemistry for Citric Acid Passivation
      • Electropolishing Solutions: Electrolyte Chemicals
      • Conversion Coating Chemistry
      • Hex Chrome Phase Out and Alternatives for Conversion Coating
  • Industries
  • Customer Testimonials
  • About Us
  • Contact Us
Contact an Expert
home Best Technology / Passivation Equipment & Ultrasonic Passivation Systems for Stainless Steel with Nitric / Citric Acid / Nitric vs. Citric Passivation of Stainless Steel and Titanium

Nitric vs. Citric Passivation of Stainless Steel and Titanium

Table of contents
  1. Nitric vs Citric Acid Passivation: What’s the Difference?
    1. Passivating Stainless Steel
    2. Passivating Titanium
  2. Nitric Acid Passivation
    1. Options for Nitric Acid Passivation in ASTM A967
  3. Citric Acid Passivation
    1. Options for Citric Acid Passivation in ASTM A967
  4. Comparison Summary: Nitric vs Citric Passivation
  5. Video: Automated Customizable Nitric and Citric Passivation System
  6. Equipment for Nitric Acid Passivation
    1. Types of passivation equipment

Nitric vs Citric Acid Passivation: What’s the Difference?

Nitric vs Citric Passivation - Aircraft partsMany people ask about the differences between nitric acid and citric acid for passivating parts made of stainless steel (SS), titanium (Ti), and other alloys. So what is the difference between nitric vs. citric passivation? Compared to the nitric acid method of passivating, citric acid passivation is:

  • Newer – Began to be adopted in the 1990s
  • More environmentally friendly – No nitrogen oxide vapors (NOx) that contribute to smog and acid rain and affect the ozone layer of the atmosphere
  • Safer – Non-hazardous material requires no special handling or regulatory oversight and does not corrode other equipment.

Passivating Stainless Steel

Both nitric acid and citric acid are effective in passivating many grades of stainless steel, and both methods are described in detail in the industry standards ASTM A967 and AMS 2700.

In the 1960s, the U.S. military defined the first specifications for passivation using nitric acid on stainless steel in the QQ-P-35 standard. Over time, however, the environmental and safety hazards of using nitric acid became more apparent. The quest for an effective, safer alternative was fulfilled with the use of citric acid passivation, which began to be adopted in the 1990s.

Industry standards for citric passivation first came to the aerospace industry, where the QQ-P-35 standard became the AMS-QQ-P-35, which was later replaced by the AMS 2700 standard in the early 2000s. For other industries such as medical device, the industry standard ASTM A967 replaced the old QQ-P-35 standard in 2005.

Since both of the most-used standards derived from the QQ-P-35 military standard of the 1960s, questions often arise about the differences between ASTM A967 vs. AMS 2700. These standards are essentially equivalent, and differ by who uses them. The aerospace industry tends to use AMS 2700, while other industries use ASTM A967.

Today both nitric acid and citric acid are widely-used, industry-accepted methods of passivation of stainless steel.

Passivating Titanium

What if you need to passivate titanium? Since titanium alloys do not contain iron, they technically do not need a passivation treatment to form a passive metal oxide layer. However, if titanium parts may have been contaminated with iron during manufacturing processes, that iron could become rust if it is not removed. The process of removing iron from the surface of titanium is essentially identical to that of passivating stainless steel, so the term passivating titanium is often applied.

While it is possible to passivate titanium with citric acid, the passivation of titanium is more typically governed by ASTM F86, which only specifies nitric acid, and not citric acid.

Nitric Acid Passivation

Nitric acid passivation is the traditional method of removing free iron from the surface of stainless steel, titanium and other metals for corrosion prevention.

As the legacy method of passivation, nitric acid on stainless steel offers the advantage of a proven, established process. For those committed to using nitric passivation, a variety of options exist to optimize performance with the particular grade of stainless steel.

Less corrosion-resistant grades of stainless steels have a greater risk of etching, also known as flash attack, during passivation in nitric acid. To reduce that risk, the following approaches may be used:

  • Addition of sodium dichromate to the nitric acid
  • Higher nitric acid concentration
  • Higher temperature of nitric acid.

Note that even though these options reduce the risk of etching, they do increase the risks to worker safety associated with hazardous chemicals. Sodium dichromate is a hexavalent chromium compound, and a known carcinogen.

Options for Nitric Acid Passivation in ASTM A967

Type Chemistry Temperature Time Best For
Nitric 1 20 – 25% nitric acid by volume,
2.5% +/- 0.5% sodium dichromate by weight
120 – 130 °F 20 min. minimum
  • Precipitation hardened
  • Martensitic
  • Free machining
  • Ferritic, except types 430 and 446
Nitric 2 20 – 45% nitric acid by volume 70 – 90 °F 30 min. minimum
  • Austenitic
  • Duplex (type 329)
Nitric 3

20 – 25% nitric acid by volume

120 – 140 °F 20 min. minimum
  • Austenitic, except high-carbon grades (304H, 316H, 321H, 347H)
  • Duplex (type 329)
  • Ferritic, except lower chromium grades (405, 409)
Nitric 4 45 – 55% nitric acid by volume 120 – 130 °F 30 min. minimum
  • Precipitation hardened
  • Martensitic, except types 416 and 420
  • Ferritic lower chromium grades (405, 409, 429)
  • Austenitic high-carbon grades (304H, 316H, 321H, 347H)
Nitric 5 Other combinations of temperature, time, nitric acid concentration and other chemicals that produce parts that pass test requirements in ASTM A967.

Nitric acid itself is a hazardous chemical that emits toxic and corrosive fumes, and therefore requires special attention to ventilation and safe chemical handling. Though not a known carcinogen, nitric acid can cause severe chemical burns rapidly. When released in the atmosphere, nitric acid emissions contribute to acid rain and smog, and can affect the ozone layer. All of this explains why the industrial use of nitric acid is highly regulated, with stringent requirements for worker safety and environmental protection.

Citric Acid Passivation

Citric acid passivation offers a safer, more environmentally friendly alternative to nitric acid passivation. Citric acid is an organic acid that comes from citrus fruits like oranges, and as such is safe for employees to handle. Fumes from citric acid are not toxic and not harmful to the atmosphere. Citric passivation meets all current industry standards, and is effective with nearly all grades of stainless steel.

In the past, some manufacturers avoided citric acid due to potential organic growth and molding issues. Today, citric acid has improved with new formulations for biocides which prevent organic growth in solution. These new advancements have allowed smaller manufacturers which had little to no experience with chemical handling to bring their passivation process in-house.

Citric passivation vs. nitric passivation also offers shorter cycle times. Parts can be processed in as little as 4 minutes when using citric acid, compared to 20 minutes minimum with nitric acid.

As with nitric acid, it is important to maintain a balance between temperature, immersion time and acid concentration with citric acid passivation, to avoid the challenges of runaway corrosion known as flash attack.

Options for Citric Acid Passivation in ASTM A967

Type Chemistry Temperature Time
Citric 1 4 – 10% citric acid by weight* 140 – 160 °F 4 min. minimum
Citric 2 4 – 10% citric acid by weight 120 – 140 °F 10 min. minimum
Citric 3 4 – 10% citric acid by weight 70 – 120 °F 20 min. minimum
Citric 4 Other combinations of temperature, time, citric acid concentration and other chemicals that produce parts that pass test requirements in ASTM A967.
Citric 5 Same as Citric 4, except the pH of the immersion bath must be maintained in the range of 1.8 – 2.2.

*Note that the citric acid percentage is measured by weight, while the nitric acid percentage is measured by volume.

For more details on citric passivation, please see our page on citric acid passivation. Learn more about citric acid material compatibility with our CitriSurf® Compatibility Guide for various grades of stainless steel.

The following chart provides a summary of the key differences between nitric vs citric passivation.

Comparison Summary: Nitric vs Citric Passivation

Nitric Acid

Citric Acid

Safety Hazardous handling required Very safe to use as directed
Air breathing Emits toxic and corrosive gases No toxic and corrosive gases emitted
Ease of use Chemical handling safety equipment and extreme care required for most use Minimum chemical handling safety equipment required
Passivation Excellent passivation of most grades of stainless steel Excellent passivation of nearly all grades of stainless steel
Environment Environmentally hazardous Environmentally friendly
Cost
  • Low cost raw material
  • High cost maintenance and disposal
  • High cost ventilation system for safe use
  • Higher cost chemistry
  • Lower maintenance, safety and waste disposal costs
  • Lower concentration of chemicals required
  • Lower overall cost to use
Passivation process duration 20 minutes to several hours 5-20 minutes typical
Process temperature
  • Elevated temperature required for many grades
  • Nitric acid very dangerous at elevated temperatures
  • Room temperature use for many grades
  • Elevated temperature expedites the process
  • Safe without ventilation
Chemical process maintenance Regular solution monitoring required (titration) Regular solution monitoring required (specific gravity)
Iron oxide removal Slowly removes iron oxides Readily removes iron oxides
Equipment Long-term corrosive degradation of non-stainless steel metal or polymer-based equipment or components No corrosive degradation of equipment
Process stability Must control time and temperature closely as danger of nitric oxide gas exists – proper ventilation required Less prone to time and temperature variation, no hazardous vapors
ASTM A967 Meets requirements Meets requirements
AMS 2700 Meets requirements Meets requirements
ASTM A380 Meets requirements as referenced in ASTM A967 Meets requirements as referenced in ASTM A967
AMS QQ-P-35 Meets requirements as referenced to AMS 2700 and ASTM A967 Now referenced to AMS 2700 and ASTM A967

To learn more about nitric vs citric passivation industry standards and specifications, please see our page "What is Passivation?"

Today, many companies are taking a second look at citric acid due to its ease of chemical handling, disposal and overall safety for employees, all of which are more challenging when going with nitric acid passivation vs citric acid passivation. Best Technology works closely with many companies in the aerospace and medical device industries and has successfully assisted these companies with converting from nitric to citric acid. Often it is as simple as talking with the end customer and showing them the equivalency of the types of passivation.

Video: Automated Customizable Nitric and Citric Passivation System
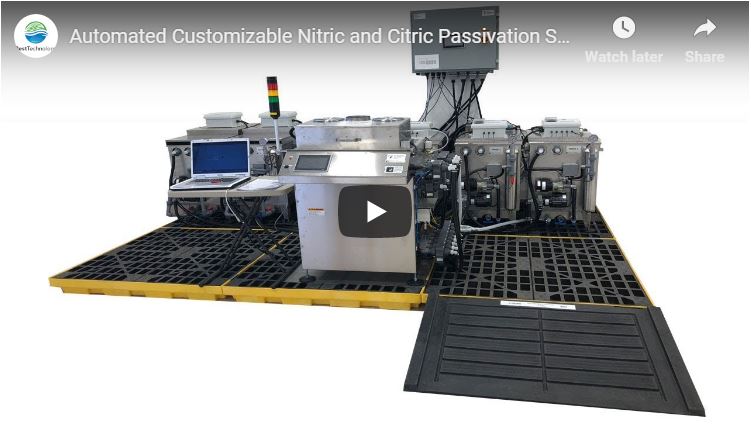
Automated Customizable Nitric and Citric Passivation System

Need BOTH nitric AND citric acid passivation? This system can handle it all. This 3-in-1 system offers 3 different automated passivation options:

  1. Nitric acid
  2. Nitric acid with sodium dichromate
  3. Citric acid.

A key advantage of an automated passivation system is that it is designed to run as a closed-loop system, so the operator is not exposed to chemicals like nitric acid.

Equipment for Nitric Acid Passivation

Best Technology is a recognized industry leader in passivation equipment, systems, tanks and lines. Our automated passivation equipment is particularly well-suited for nitric acid passivation, due to reduced worker interaction with hazardous chemicals. Whether it's citric acid or nitric acid passivation, Best Technology can provide a system that's right for your company.

Types of passivation equipment

  • Small benchtop passivation equipment
  • Wet bench passivation equipment
  • Automated passivation systems
  • Agitated immersion passivation systems

Except as noted, each of these types of passivation equipment can be built for use with either citric acid or nitric acid. The nitric acid systems do require additional ventilation in the system design, so it’s important to understand which chemistry you’ll be using when specifying passivation equipment.

CitriSurf® is a registered trademark of Stellar Solutions, Inc. McHenry IL USA.

Consult an expert

Need advice on nitric vs citric passivation, or planning your passivation line? Exploring making the move from nitric acid to citric acid? We can help. Contact a passivation expert at Best Technology to learn more.
Latest News & Products from Best Technology

BestSolv Novec Replacements

Running Out of 3M™ Novec™ Stock? How to Transition to Your BestSolv® Replacement Path

Don’t let running out of 3M™ Novec™ stock become a concern. As 3M™ Novec™ Engineered Fluids moved toward discontinuation, manufacturers took different approaches to maintaining process continuity. Some transitioned to alternative fluids, while others secured additional inventory and continued operating with the chemistry already qualified in their process. If your operation is still using remaining Novec™ stock, [...]

Read More

Read More

Trusted By Thousands of Customers Since 1992

  • Industrial Parts Washers
    • Products
      • Agitated Immersion Heated Parts Washer
      • Automatic Parts Washer System with Conveyor
      • Phosphating Lines
      • Automated Phosphate Lines for High-Volume Powder Coat Pre-Treatment
      • Oil Removal Systems
    • Case Studies
      • Pipe Washing Equipment
      • Designing a Phosphate Line for Today’s Process and Tomorrow’s Needs
      • Machine Shop Parts Washer for True Oil
      • Automotive Parts Washer System
  • Ultrasonic Cleaning Systems
    • Product Information
      • How Clean is Clean?
      • How Do Ultrasonic Cleaners Work?
      • What is an Azeotrope?
    • Products
      • Benchtop Ultrasonic Cleaner
      • Benchtop Ultrasonic Parts Cleaning Multi-Tank Systems
      • Ultrasonic Cleaning Consoles
      • Automated Ultrasonic Parts Cleaning Equipment Wash-Rinse-Dry
      • Automated Ultrasonic Cleaning System for High-Volume Production
      • Large Ultrasonic Parts Cleaner with Agitated Immersion
      • Immersible Ultrasonic Transducers
      • Vapor Degreasing Systems
      • Vapor Degreasers
    • Case Studies
      • Automated Pickling and Cleaning System Case Study
      • Automated Ultrasonic Injection Mold Cleaner System
      • 3D Printer / FDM Parts Post Process Ultrasonic Cleaning
      • Machine Shop Parts Washer for Swiss and CNC Precision Parts
      • Vapor Degreaser for Medical Device Instruments
  • Passivation Equipment
    • Product Information
      • What is Passivation? How Does It Work?
      • Nitric vs. Citric Acid Passivation
      • Passivation with Citric Acid
      • What Is Pickling of Stainless Steel? How Do Descaling, Pickling and Etching Work?
      • Passivation Cost Savings Calculator
    • Products
      • Benchtop Ultrasonic Passivation Equipment
      • Passivation Wet Bench for Citric / Nitric Acid
      • Ultrasonic Automated Passivation Equipment
      • Automated Passivation Systems for High-Volume Production
      • Agitated Immersion Multi-Tank Passivation Systems
      • Salt Fog and Humidity Test Chambers for Reliable Corrosion and Environmental Testing
    • Case Studies
      • Case Study: Bringing Citric Acid Passivation In-House for Stainless Steel Medical Device Parts
      • Automated Ultrasonic Passivation System for Medical Device Parts
      • Cleanroom Space Saving Automated Passivation System
      • Heated Polypropylene Passivation and Rinse Tanks
      • Applicable Articles
  • Electropolishing Equipment
    • Product Information
      • What is Electropolishing? How Does Electropolishing Work?
      • Electropolishing Cycle and Current Calculator
      • Passivation vs. Electropolishing
    • Products
      • Tabletop Electropolishing Equipment & Electropolishing Machines
      • Electropolishing Wet Benches
      • Semi-Automated Electropolishing Systems for High-Volume Production
      • Large Scale Part Electropolishing Systems
    • Case Studies
      • EP System – Open Top Wet Bench with Spray Rinse
  • Surface Finishing Systems
    • Alodine Lines
      • Chem Film Equipment for Chromate Conversion Coating
      • What is Alodine® / Chem Film / Chromate Conversion Coating?
      • Alodine Chem Film Tank Line
      • Ready to Set Up a Chem Film (Alodine) Line?
      • Automated Chem Film (Alodine) Systems
      • Hex Chrome Phase Out and Alternatives for Conversion Coating
      • Salt Fog and Humidity Test Chambers for Reliable Corrosion and Environmental Testing
    • Mass Finishing Machines
      • Centrifugal Barrel Finishing Machines
      • Vibratory Bowl Polishers
    • Titanium Anodizing
      • Titanium Anodizing Systems
      • What is Titanium Anodizing?
      • Titanium Anodizing Equipment
  • Automation Systems
    • Product Information
      • What Is Process Automation for Metal Finishing?
    • Products
      • Rail-Mounted Gantry Crane Automation
      • Automated Passivation Systems for High-Volume Production
      • Automated Chem Film (Alodine) Systems
      • Semi-Automated Electropolishing Systems for High-Volume Production
      • Automated Ultrasonic Cleaning System for High-Volume Production
      • Automated Phosphate Lines for High-Volume Powder Coat Pre-Treatment
      • Ultrasonic Automated Passivation Equipment
    • Case Studies
      • Automated Passivation for High-Volume Production: Case Study
      • Automated Pickling and Cleaning System Case Study
  • Wet Benches
    • Product Information
      • What is a Fume Hood? How Do Fume Hoods Work?
    • Products
      • Fume Hoods
      • Wet Benches for Semiconductor & FM4910 Applications
      • Wet Benches for Citric / Nitric Passivation of Stainless Steel and Titanium
      • Wet Benches for Electropolishing
      • Cascade Overflow Rinse Tanks
      • Quick Dump Rinse Tank
    • Case Studies
      • Semiconductor Chemical Processing Wet Bench and Fume Hood
  • Specialty & Custom Industrial Process Systems
    • Products
      • Automated Chemical Neutralization Tank Cart
      • Salt Fog and Humidity Test Chambers
      • Vapor and Dryfilm PTFE Coating Systems
      • Heated Hot Air Parts Dryer
      • Solvent Recovery Equipment
  • Chemicals, Solvents & Fluids
    • Precision Cleaning Solvents
      • BestSolv® Engineered Fluids
      • Solvent Cleaning with BestSolv® Engineered Fluids
      • 3Mâ„¢ Novecâ„¢ Replacement Fluids
    • Aqueous Cleaning
      • Aqueous Cleaning Solutions: Alkaline Cleaners
    • Surface Finishing Chemicals
      • CitriSurf Passivation Chemistry for Citric Acid Passivation
      • Electropolishing Solutions: Electrolyte Chemicals
      • Conversion Coating Chemistry
  • Process Validation Templates
  • Equipment Financing
Best Technology applications engineer

Connect with Our
Experts Today!

Ready to boost your manufacturing process efficiency?

Our expert team is just a click away. Reach out now to get personalized advice on choosing the best system for your specific needs. Let's enhance your operations together!

Contact an Expert
Best Technology Inc.

Best Technology Inc.
14040 23rd Avenue N.
Minneapolis, MN 55447

phone icon612.392.2414

Follow Us
  • Facebook icon
  • X icon
  • LinkedIn icon
  • YouTube icon
  • Pinterest icon

Quick Links

  • Product Line Card
  • Case Studies
  • Videos
  • Site Map
  • Equipment Financing
  • Contact Us

Products

  • Industrial Parts Washers
  • Ultrasonic Cleaning Systems
  • Passivation Equipment
  • Electropolishing Equipment
  • Surface Finishing Systems
  • Chemistries, Solvents & Fluids

Industries Served

  • Medical Device
  • Aerospace
  • Electronics
  • Automotive
Contact an Expert

Copyright © 2026 · Best Technology Inc. · Privacy Policy

Precision Cleaning, Passivation & Finishing Systems
Contact an Expert
612.392.2414
  • facebook
  • Twitter
  • LinkedIn
  • YouTube
  • Pinterest

"*" indicates required fields

1Contact Info
2Your Project

Start Here for the Best Solution

Are you looking to purchase equipment?*
Note: We specialize in custom metal finishing equipment and do not offer job shop or contract services.
Best Technology designs custom metal finishing equipment for commercial manufacturing environments. Hobby, student, or consumer projects are not supported.
Are you looking for budgetary pricing or a formal quote?
How soon are you looking to purchase equipment?
Has this project received internal approval at your organization?
Are you currently doing this process in-house or sending it out to a vendor?