

When a manufacturer needs to prepare metal parts for coating, painting, or another downstream finishing process, a phosphate stage might be one part of the equation. The parts must first be cleaned properly, the chemistry must operate under controlled conditions, rinsing must be incorporated at the right points, and the equipment needs to support a repeatable process from one production run to the next.
That was the challenge behind a recent custom phosphate line engineered by Best Technology. The manufacturer needed a system capable of supporting its current zinc phosphate process, but the equipment also needed to account for a future manganese phosphate stage. Rather than treating those as two separate equipment projects, Best Technology designed the line around the manufacturer’s immediate production requirements while creating a path for the process to expand later.
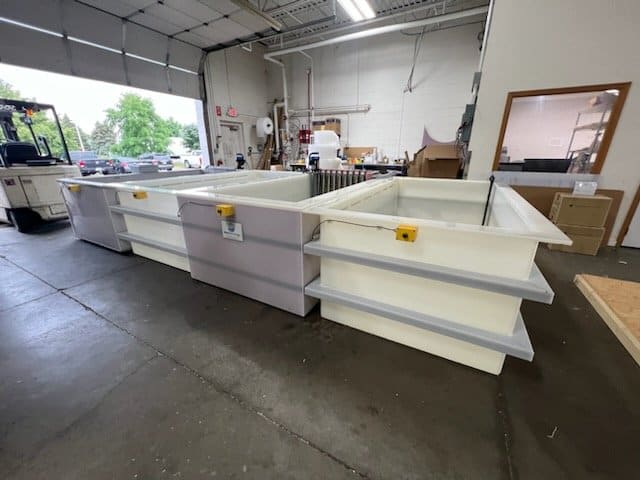
The result was a multi-stage phosphate processing system that brought cleaning, rinsing, phosphating, temperature management, circulation, filtration, containment, and centralized controls together into one coordinated line.
What Is a Phosphate Line?
A phosphate line is a series of tanks or processing stations used to clean metal parts and apply a thin phosphate conversion coating to their surfaces. A typical line may include cleaning, rinsing, phosphating, additional rinsing, and other stages depending on the part material and the requirements of the downstream process.
In simple terms, the phosphate process prepares the surface of the metal for what comes next.
For example, a manufacturer preparing steel components for powder coating does not want oil, grease, rust, machining residue, or other contamination trapped underneath the finished coating. Those contaminants can interfere with adhesion and contribute to inconsistent finishing results. Cleaning and phosphating establish a more controlled surface before the part reaches the coating operation.
Phosphating is one type of chemical conversion coating, meaning the treatment chemically modifies the surface rather than simply depositing a separate layer of material on top of it. Best Technology designs phosphating systems for processes including iron and zinc phosphate conversion coatings.
The Manufacturing Challenge: More Than Four Tanks
The initial requirement for this project called for a four-stage immersion line.
The process sequence was:
- Alkaline cleaning
- Water rinsing
- Zinc phosphating
- Final water rinsing
On paper, that sequence looks straightforward. In practice, however, the effectiveness of the phosphate process depends on what happens inside and between those stages.
The first tank had to remove contamination from the metal before phosphating. The cleaning solution needed to operate at an elevated temperature and required circulation and filtration. The phosphate stage also required controlled heating, circulation, filtration, and water addition. Rinse tanks had to remove chemistry carried over from the preceding process before the parts moved forward.
This is why a phosphate line is not simply a collection of tanks.
A successful system must be designed around the parts being processed, the chemistry being used, the required operating temperatures, process sequence, facility utilities, tank construction, production workflow, and future manufacturing requirements.
That same principle applies more broadly when selecting industrial parts washing and cleaning equipment. Part geometry, contamination, chemistry, throughput, cleanliness requirements, and the downstream process all influence how a cleaning or surface-preparation system should be configured.
Building the Cleaning Stage Into the Phosphate Process
Before a metal surface can be phosphated successfully, it first needs to be in the appropriate condition for the conversion coating to form.
For this system, that process begins with a heated alkaline cleaning stage.

The purpose of the cleaning tank is to remove contaminants that would otherwise interfere with subsequent surface treatment. Depending on the manufacturing process, parts entering a phosphate line may carry oils, grease, rust, particulate, or residues from previous operations.
The customer’s cleaning tank was designed with controlled heating, solution circulation, filtration, and low-level monitoring. These functions support the cleaning chemistry while helping maintain more consistent operating conditions.
This principle is also used throughout industrial parts cleaning. Agitated and heated immersion parts washers combine chemistry, temperature, fluid movement, and filtration to improve cleaning performance, particularly when parts have complex surfaces or heavier contamination.
The goal is not simply to make the part look clean. The surface needs to be appropriately prepared for the next manufacturing step.
Why the Rinse Stages Matter
After cleaning, the parts enter a water rinse before moving into the phosphate tank.
That intermediate rinse helps reduce carryover of alkaline cleaning chemistry into the phosphate bath. After phosphating, another rinse removes residual phosphate solution before the parts continue into the next operation.
Separating these process stages helps maintain the intended chemistry in each tank.

This is particularly important with zinc phosphate because cleaning and phosphating are normally performed as separate operations. A wash-rinse-zinc phosphate-rinse configuration is therefore a common approach for this type of process.
The rinse stages may appear less technically significant than the heated process tanks, but they support the stability of the entire line. Every stage affects the conditions of the stage that follows it.
Applying the Zinc Phosphate Conversion Coating
After cleaning and rinsing, the parts enter the zinc phosphate tank.
Zinc phosphate forms an adherent crystalline conversion coating on the metal surface. The coating can provide a better foundation for subsequent finishing processes while also helping support corrosion resistance.
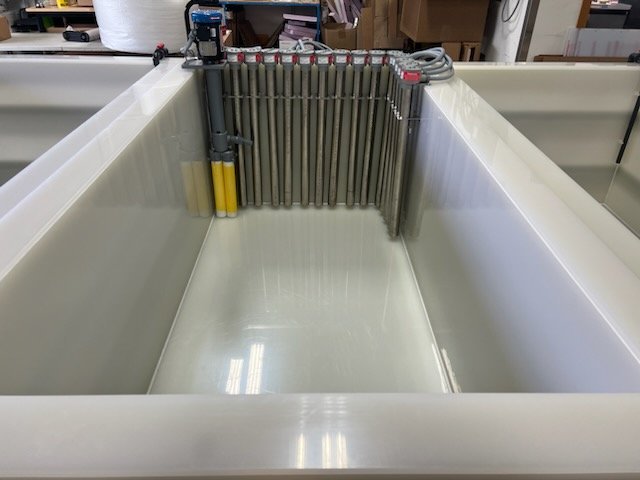
Several variables influence phosphate coating performance, including process time, temperature, chemical concentration, and pH. Because these variables affect the chemical reaction taking place at the metal surface, maintaining stable process conditions is important when manufacturers are trying to produce consistent results from load to load.
For this project, the phosphate tank therefore incorporated controlled heating, circulation, filtration, water addition, insulation, and level monitoring.
Rather than relying on an operator to independently manage each component of the system, these functions were integrated into the overall equipment and control architecture.
Bringing the Process Together Through Centralized Controls
As a processing line becomes more complex, the control system becomes increasingly important.
The completed phosphate line incorporates a programmable logic controller, commonly called a PLC, along with a remote 10-inch color touchscreen. From the interface, an operator can access the process controls for the line, monitor temperatures, adjust temperature settings, review alarms and alarm history, and access troubleshooting information.

A seven-day timer also allows the line to be scheduled to begin heating automatically.

That capability can be particularly useful for heated chemical processes. Instead of arriving at the beginning of a shift and waiting for a large process bath to reach its operating temperature, the heating schedule can be coordinated with planned production.
The controls do not replace the need for proper process management. They give operators a centralized way to manage the equipment that supports that process.
As manufacturing volume increases, more extensive automation can also be incorporated. Best Technology designs automated phosphate coating systems that automatically move baskets or racks through process stages to improve throughput, reduce manual handling, and provide tighter control over tank sequencing and dwell times.
The appropriate level of automation depends on production volume, part handling requirements, process complexity, available labor, and the degree of repeatability the manufacturer needs.
Designed for a Process That Continues to Evolve
One of the most important requirements became what the manufacturer would need after the initial system was installed.
The immediate process called for zinc phosphating. The final equipment design, however, also accounted for an additional manganese phosphate tank that would arrive later.
That future tank was planned to fit between the zinc phosphate stage and the final rinse.
This requirement influenced the system differently than simply adding another tank after installation. The line needed to be designed from the beginning with the future process stage in mind.
That is an important consideration for manufacturers evaluating new process equipment.
Production requirements rarely remain completely static. A facility may add a new coating specification, take on a different family of parts, increase throughput, introduce automation, or add another chemical process.
Replacing an entire line every time the manufacturing process changes is rarely desirable. Having a flexible line keeps costs down and it’s overall more efficient.
When future requirements are reasonably foreseeable, incorporating them into the initial engineering discussion can make later modifications significantly more practical. That is why Best Technology works closely with customers to understand not only what the process needs today, but also how those requirements may change over time. Clear communication during the design stage helps ensure the finished system is built around the customer’s specific process, facility, and production needs.
In this case, Best Technology was able to provide the zinc phosphate processing capability the manufacturer required immediately while designing the final line so the planned manganese phosphate stage could become part of the process later.
Zinc Phosphate and Manganese Phosphate Serve Different Needs
Zinc and manganese phosphate are both phosphate conversion coatings, but they should not automatically be treated as interchangeable processes.
Zinc phosphate is commonly used when a manufacturer needs a phosphate surface that supports coating adhesion and corrosion protection. It is frequently associated with pretreatment before painting or powder coating.
Manganese phosphate is generally selected for different performance requirements, particularly applications where the phosphate coating contributes to wear resistance, friction characteristics, or oil retention on ferrous components.
The correct phosphate chemistry therefore depends on what the finished component needs to do.
This is another reason the application should drive the equipment design. Tank construction, heating requirements, chemistry, filtration, process sequence, rinsing, and controls all need to support the actual surface-finishing objective.
A manufacturer should begin with the required result and work backward into the process and equipment needed to achieve it.
Where Phosphate Lines Can Be Used

Phosphate processing is used across a wide range of industries because many manufactured metal products require controlled surface preparation before they are coated, painted, assembled, lubricated, or placed into service.
A phosphate line may be appropriate for parts such as:
- Automotive and transportation components
- Metal brackets and fabricated assemblies
- Machinery and equipment components
- Welded steel fabrications
- Frames, housings, and enclosures
- Agricultural and construction equipment components
- Industrial hardware and fasteners
- Metal cabinets and electrical enclosures
- Components that will later be painted or powder coated
- Ferrous parts requiring a conversion coating before another finishing step
The exact sequence depends on the material, contamination, phosphate chemistry, downstream coating, corrosion requirements, production volume, and applicable specifications.
For powder coating applications in particular, surface preparation can have a significant effect on the finished result. Best Technology’s phosphate wash and conversion coating lines for powder coat preparation are designed around multi-stage processes that can incorporate cleaning, rinsing, phosphating, and additional treatment stages as required by the application.
Equipment and Chemistry Need to Be Considered Together
A well-built process tank cannot compensate for inappropriate chemistry, and the right chemistry cannot compensate for equipment that cannot maintain the process conditions it requires.
The two need to work together.
This is particularly important in surface finishing, where variables such as temperature, solution movement, chemistry concentration, contamination, rinsing, dwell time, and part condition can interact.
Best Technology approaches these applications from both sides of that equation. We supply industrial parts washers and process equipment as well as cleaning and surface-finishing chemistries. That allows an application to be considered as a complete manufacturing process rather than treating the tank, controls, and chemistry as unrelated components.
The objective is not simply to sell equipment capable of holding a chemical solution. It is to understand what needs to happen to the part and configure the process equipment around that requirement.
What Manufacturers Should Consider When Planning a Phosphate Line
This project demonstrates several questions worth answering before specifying a new phosphate processing system.
What contamination is present on the incoming parts? What cleaning process will remove it? Which phosphate conversion coating is appropriate for the required finish? What operating temperatures does the chemistry require? How will chemistry carryover be controlled between tanks? How large are the parts and production loads? How will operators handle those loads? What process variables need to be monitored? And, importantly, what could change in the next several years?
Those questions determine much more than tank dimensions.
They determine how the entire line should function.
For this manufacturer, the answer was a custom system combining heated alkaline cleaning, rinsing, zinc phosphating, filtration, circulation, temperature management, containment, and centralized controls, while leaving a defined path for manganese phosphate capability to be incorporated later.
That is the larger lesson from the project.
A phosphate line should not be designed only around the equipment a manufacturer wants to purchase today. It should be designed around the process the manufacturer needs to control, with enough understanding of future requirements to avoid unnecessary limitations tomorrow.
Best Technology designs phosphating lines, industrial parts washing systems, and custom process equipment around the specific parts, chemistry, production requirements, and finishing objectives of each application.
Best Technology designs phosphate lines around the specific parts, chemistry, process requirements, and production goals of each application. If you are planning a new phosphate line or evaluating changes to an existing surface-preparation process, connect with a phosphate treatment and parts cleaning expert to discuss your application and the system requirements that may be the best fit.

 612.392.2414


